Passive Acoustic Emission Sensing Principles
While conventional predictive maintenance relies exclusively on vibration sensors for rotating machinery, static vessels and pipelines do not vibrate until they are on the verge of rupture. In our AI platform, Acoustic Emission (AE) serves as our proprietary physical sensing advantage: whenever steel under operational stress undergoes micro-crack propagation, active dislocation movement, or corrosion oxide rupture, it abruptly releases stored elastic strain energy.
This energy radiates outwards through the structure as a high-frequency transient mechanical stress wave. This physical phenomenon is known as Acoustic Emission (AE).
Unlike traditional ultrasonic testing (UT), where a technician sends an active sound wave into the metal and measures the reflection, Acoustic Emission is passive listening. The asset itself generates the sound when it is under operational stress. If a crack isn't growing, there is no sound. But the moment a crack extends by even a fraction of a millimeter under pressure or thermal load, it broadcasts an acoustic signature.
Acoustic Emission vs. Vibration Analysis
Plant engineers frequently ask: "We already have vibration sensors on our plant pumps. Why can't we just stick vibration sensors on our storage tanks and reactors?"
The table below explains why vibration analysis is the wrong tool for static structures, and why Acoustic Emission is required.
| Parameter | Updem Acoustic Emission (AE) | Traditional Vibration Analysis |
|---|---|---|
| Primary Asset Type | Static Assets: Storage tanks, pressure vessels, reactors, steam headers, pipelines. | Rotating Machinery: Pumps, motors, gearboxes, turbines, bearings. |
| Frequency Bandwidth | 30 kHz to 750 kHz (Ultrasound). Far above human hearing and plant mechanical hum. | 1 Hz to 10 kHz (Low frequency mechanical displacement and harmonics). |
| What It Detects | Active crack growth: Micro-fractures, crystal slip, active pitting corrosion, and pressurized leaks. | Mechanical motion: Unbalance, misalignment, bearing looseness, resonance. |
| What a Static Tank Does | A static tank doesn't shake or vibrate. But its steel plates generate continuous AE bursts when cracking under hydrostatic load. | A stationary tank produces zero measurable vibration until a catastrophic breach occurs. |
| Early Warning Window | 14 to 30+ Days (Detects defect at the incubation and micro-fracture stage). | 2 to 5 Days (Detects bearing spall once metal has already begun disintegrating). |
How We Filter Background Plant Noise
Real industrial plants are noisy environments: heavy pumps rumble, steam hisses through valves, product flows create pipe friction, and rain impacts tank roofs. If an acoustic system triggered on every noise, maintenance teams would disable it within three days due to false alarm fatigue.
Updem solves this challenge through a multi-stage physical and digital filtering architecture:
Mechanical Resonant Tuning
Our piezoelectric crystal elements have mechanical resonance peaks tuned between 150 kHz and 300 kHz. Low-frequency plant rumble (sub-20 kHz) cannot mechanically excite the transducer crystal.
Transient Burst Pattern Discrimination
Continuous fluid flow produces steady-state Gaussian white noise. In contrast, an authentic crack burst is an abrupt, high-energy transient spike with sharp rise times (< 5 µs) and exponential decay. Our edge processor separates them in real-time.
ASTM E1316 & ISO 12716 Acoustic Emission Burst Architecture
Standardized transient feature extraction: click any parameter below to inspect its physical definition and diagnostic significance.
Delta-T Defect Triangulation
Because sound waves propagate through steel at a known velocity (~3,200 m/s for plate waves), a crack burst reaches nearby sensors at slightly different microsecond arrival times.
By calculating the difference in arrival times (Δt) across a cluster of three or four transducers positioned around a tank bottom or vessel circumference, Updem's localization algorithms calculate hyperbolic intersection coordinates.
The maintenance team receives an exact coordinate: "Defect cluster located at Tank 104, weld seam 4, height 1.2m, angle 134°." When your team does enter the vessel during turnaround, they walk straight to the defect without having to scan the entire 1,500 square meters of steel.
Interactive Delta-T Defect Triangulation
Click anywhere on the tank shell below to simulate an acoustic crack event and observe acoustic wave propagation.
From Monpod™ Edge Sensors to Cloud Predictive Platform
Continuous acoustic emission monitoring produces massive data volumes: sampling at 1 MS/s generates gigabytes of raw data per hour. Storing raw acoustic waveforms in standard industrial databases causes massive network congestion and database bloat.
Updem solves this with a balanced two-tier architecture developed specifically for heavy industrial static infrastructure:
Autonomous Acoustic Capture & Feature Extraction
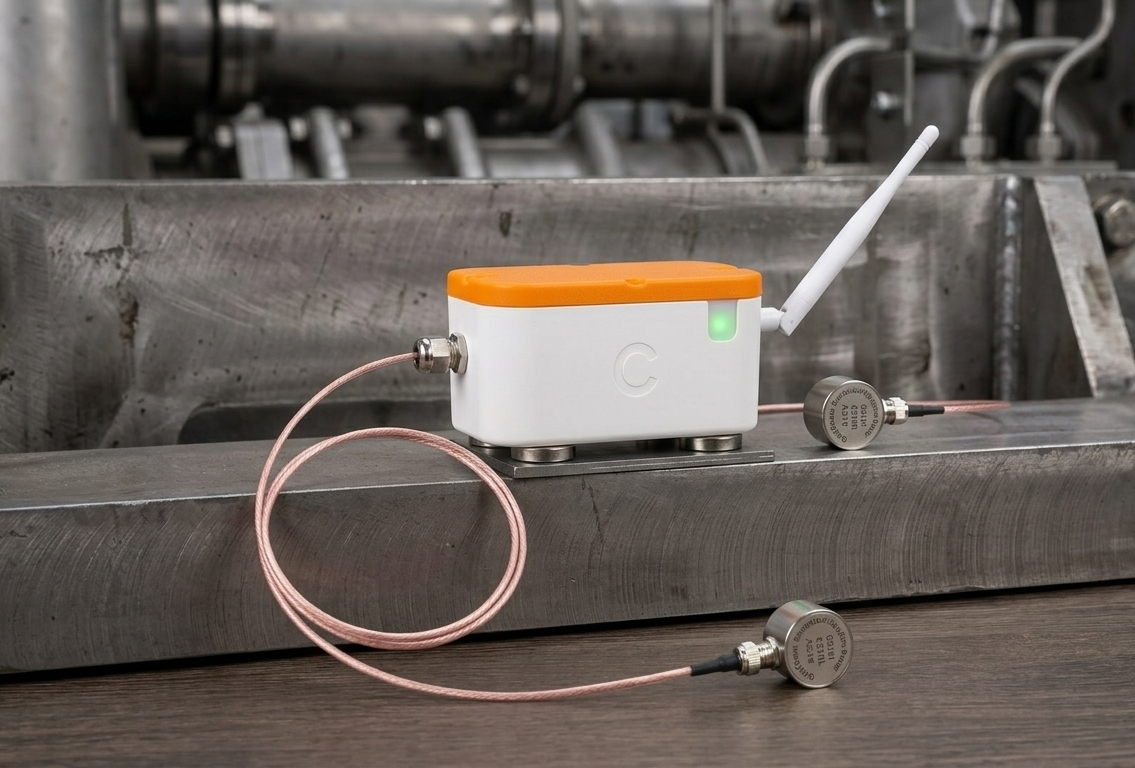
The Monpod™ is an autonomous, battery-powered wireless module that magnetically attaches to tanks, pipes, and vessel shells. It connects to dual differential piezoelectric transducers that listen in the 100 kHz to 1 MHz ultrasound band.
- Zero Hot Work: High-holding neodymium magnetic feet clamp in under five minutes without shutdown.
- Edge Extraction: Computes rolling physical features (MARSE energy, peak amplitude, duration, hit rate, RMS) right on the device.
- Wireless MQTT Telemetry: Transmits clean low-rate scalar telemetry over LoRaWAN or cellular directly to the cloud.
Predictive Maintenance & Explainable Alarms
The Updem Cloud Platform manages your asset hierarchy (mapping tanks, reactors, and pipeline segments) and provides continuous predictive intelligence.
- Learned Baselines: Automatically characterizes normal acoustic behavior for each asset during steady-state operation.
- Explainable Anomaly Detection: Detects physical feature drift before failure, stating exact causes: "AE energy and hit rate rose 4x above baseline over 6 hours."
- Closed-Loop Feedback: Maintenance engineers confirm or dismiss alerts with a single click, turning field expertise into verified training labels.
Connect Any Sensor via MQTT, HTTPS, OPC UA, and Modbus
While our Monpod modules provide dedicated high-frequency acoustic monitoring for static equipment, the Updem Cloud Platform is protocol-agnostic. Plant operators can connect existing rotating machinery sensors, process instrumentation, and third-party transmitters into a single unified predictive maintenance interface:
Engineered for High-Consequence Manufacturing Infrastructure
Passive acoustic emission and multi-sensor edge intelligence excel where conventional vibration sensors and periodic manual NDT fail: high-tonnage cyclic stresses, pressurized chemical boundaries, and superheated steam utilities.
Automotive Stamping Presses & Forging Lines
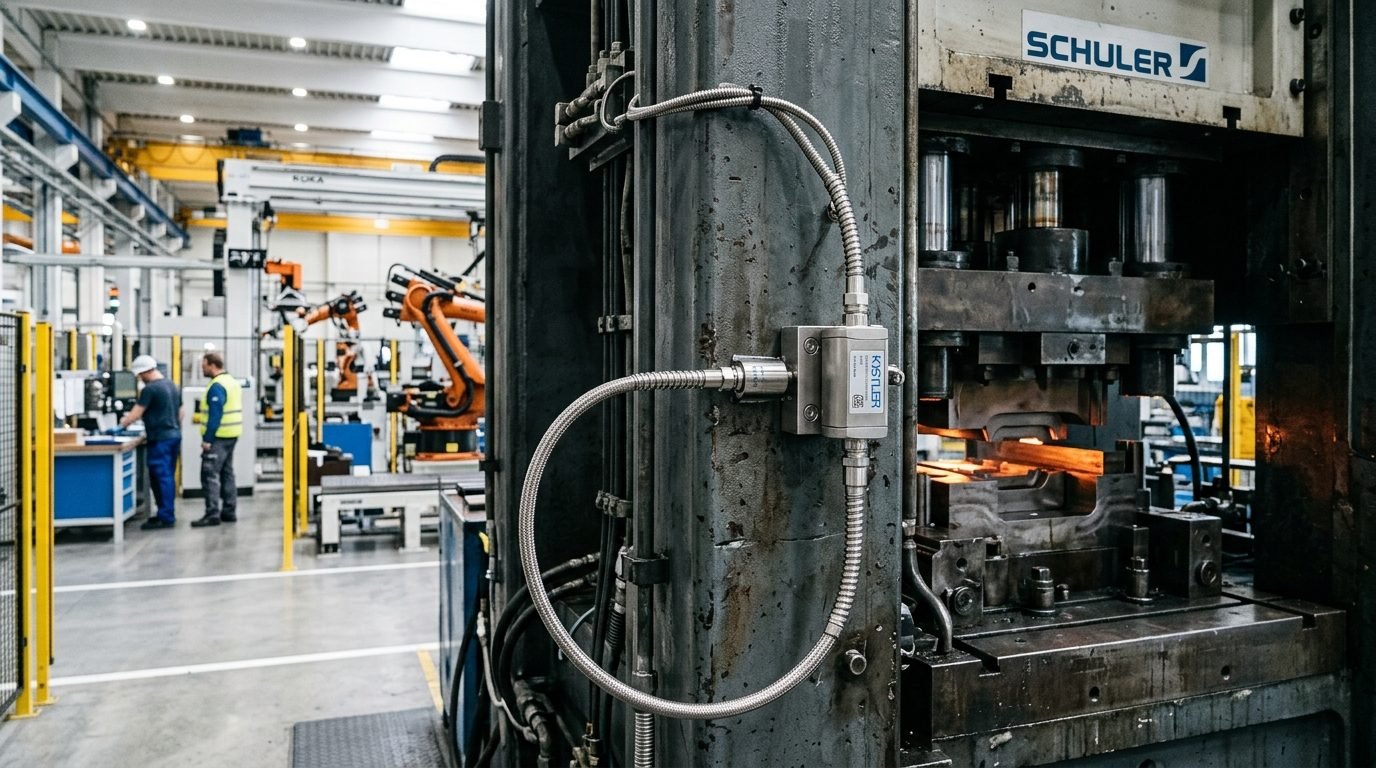
High-tonnage stamping presses (1,000T to 5,000T) cycle millions of strokes under extreme cyclic fatigue. Tie-rods, crowns, and bolster beds endure microscopic stress concentrations that nucleate fatigue micro-fissures months before sudden catastrophic mechanical fracture.
Primary Engineering Challenges Solved:
- Pre-Stressed Tie-Rod Micro-Crack Detection: Capture acoustic stress wave bursts at thread roots and column shoulders 18 to 30 days before fracture.
- High-Pressure Hydraulic Valve Block Micro-Leaks: Ultrasonic hiss separation detects internal spool leakage down to 0.1 L/min before pressure decay alters stamp depth.
- Non-Intrusive Magnetic Clamping: Magnetically attaches to press frames in under 4 hours with zero modification, zero drilling, and zero production interruption.
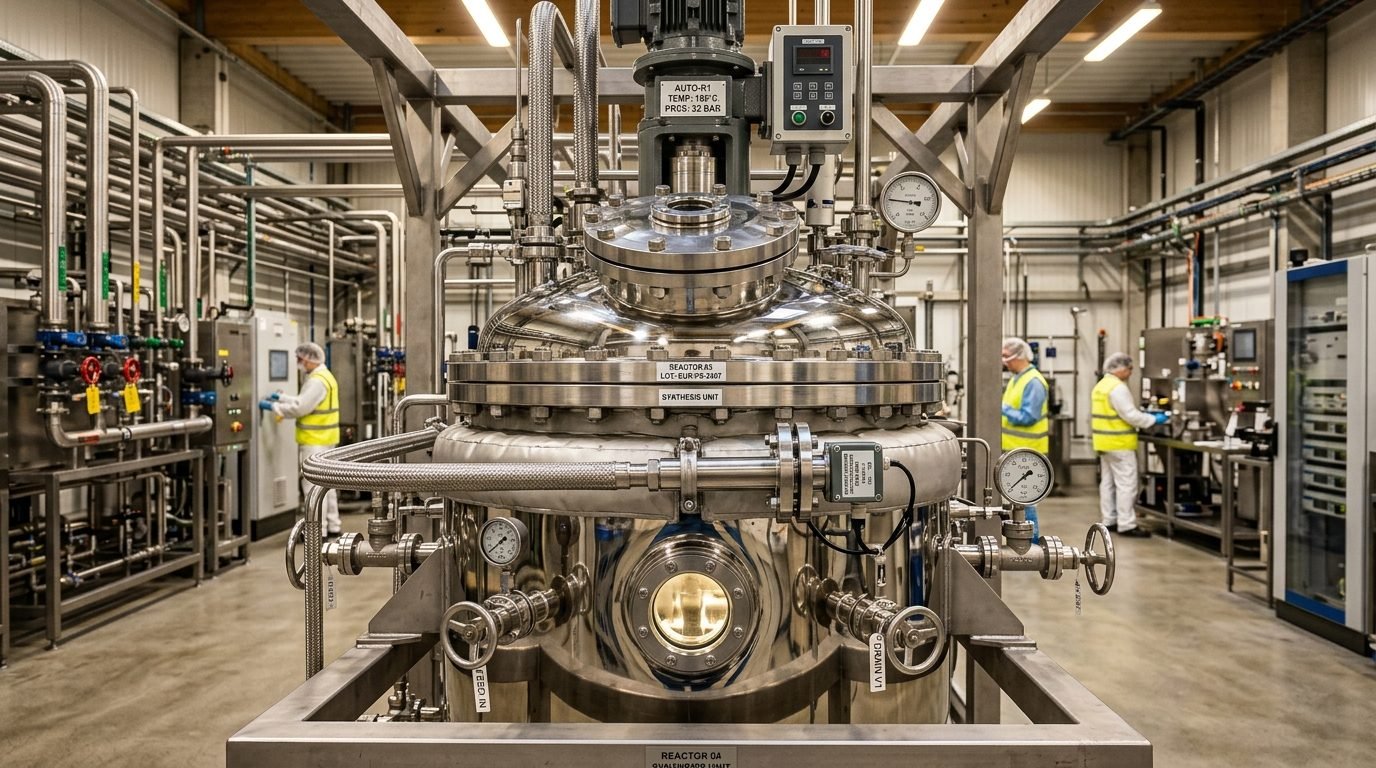
Chemical Synthesis Autoclaves & Batch Reactors
Operating high-pressure polymerization autoclaves and exothermic batch vessels requires continuous structural surveillance. Stress Corrosion Cracking (SCC) and thermal cycle fatigue initiate at microscopic grain boundaries and propagate rapidly under high pressures up to 150 bar.
Primary Engineering Challenges Solved:
- Real-Time SCC & Fatigue Detection: Detect crack tip dislocation bursts during live exothermic cycles rather than relying on multi-year manual shutdowns.
- Eliminating Confined Vessel Entry: External non-intrusive transducers grade shell and nozzle integrity without draining, purging, or sending personnel into hazardous vessel interiors.
- ASME Section VIII & PED Conformance: Physics-informed acoustic data provides auditable compliance records for operating interval extensions.
Industrial Process Steam Loops & Plant Boilers
In continuous process manufacturing (paper & pulp, chemical plants, food processing), superheated steam loops and boiler conduits operate under extreme thermal ramping. Cyclic operation drastically accelerates weld creep and micro-fissuring at high-temperature chrome-moly junctions.
Primary Engineering Challenges Solved:
- Superheated Steam Waveguide Isolation: Solid 316L waveguides mechanically isolate acoustic crystals from +500°C pipe walls while maintaining microsecond signal fidelity.
- Prevent Sudden Boiler Header Ruptures: Detect micro-fissure bursts and weld creep weeks before a catastrophic rupture shuts down the entire plant utility grid.
- Instant Acoustic Micro-Leak Pinpointing: Triangulate high-pressure steam valve and flange leaks to within ±30 cm, preventing energy waste and burn hazards.